

Blog: Insights & Updates
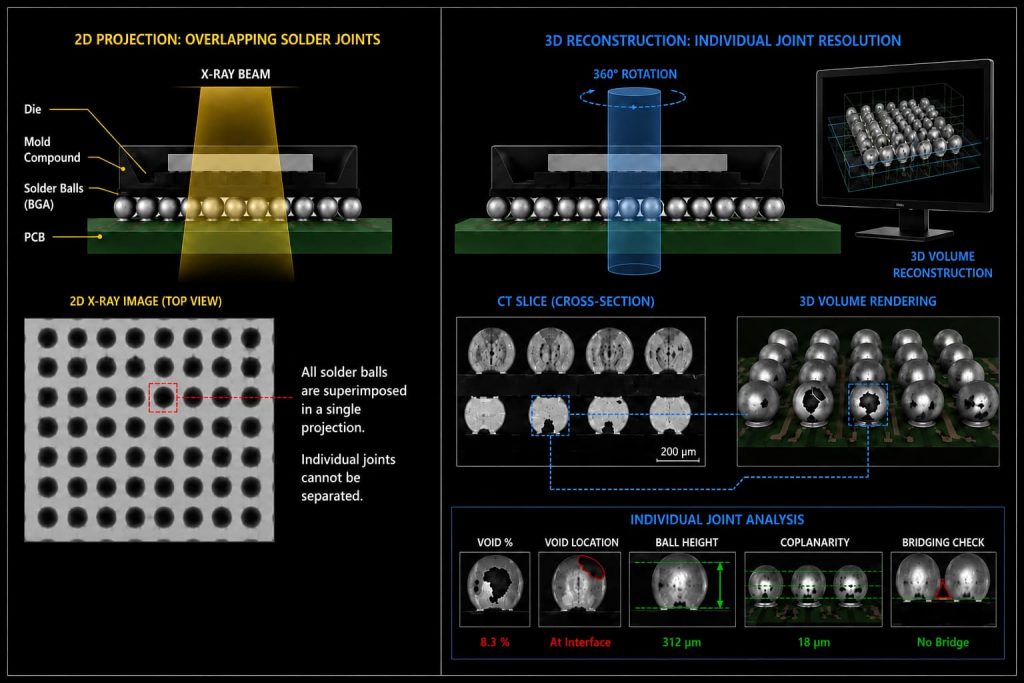
A Ball Grid Array package hides its solder connections underneath the die itself. There is no angle from which a camera, or even a standard 2D X-ray, can view a BGA joint without every other joint in the array overlapping it in the same projection.
3 minutes read
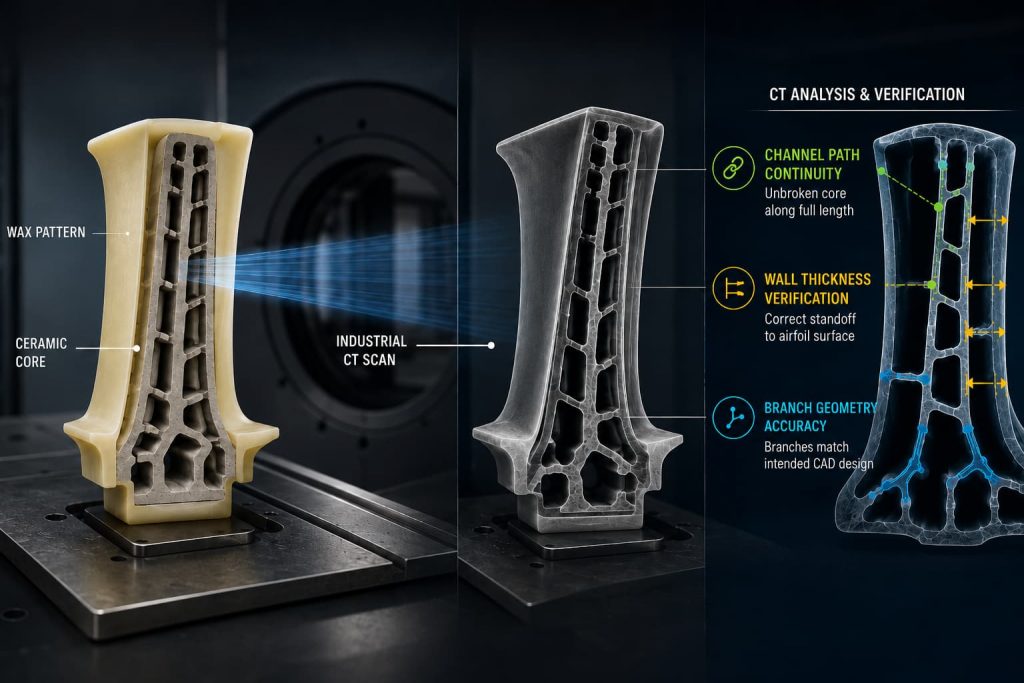
A turbine blade’s internal cooling channels are designed into the wax pattern and ceramic core long before any metal is poured.
3 minutes read
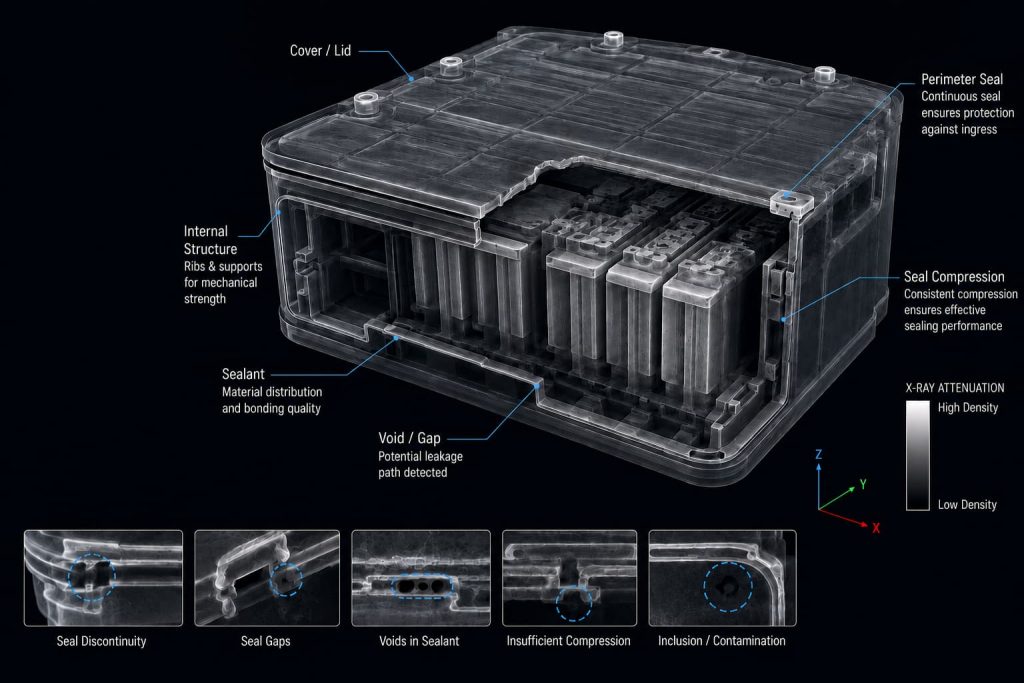
A battery pack enclosure that clears its manufacturing leak test is not guaranteed to remain sealed over its service life.
3 minutes read
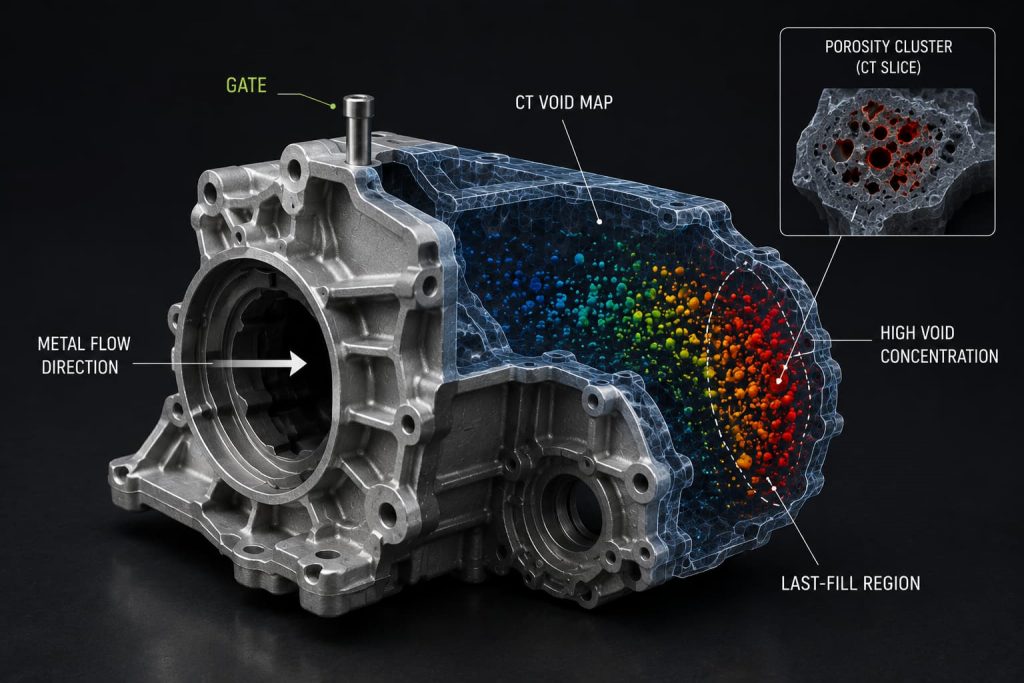
CT void analysis answers a question standard porosity inspection does not: not just how many voids exist in a casting, but where they cluster relative to the gate.
2 minutes read
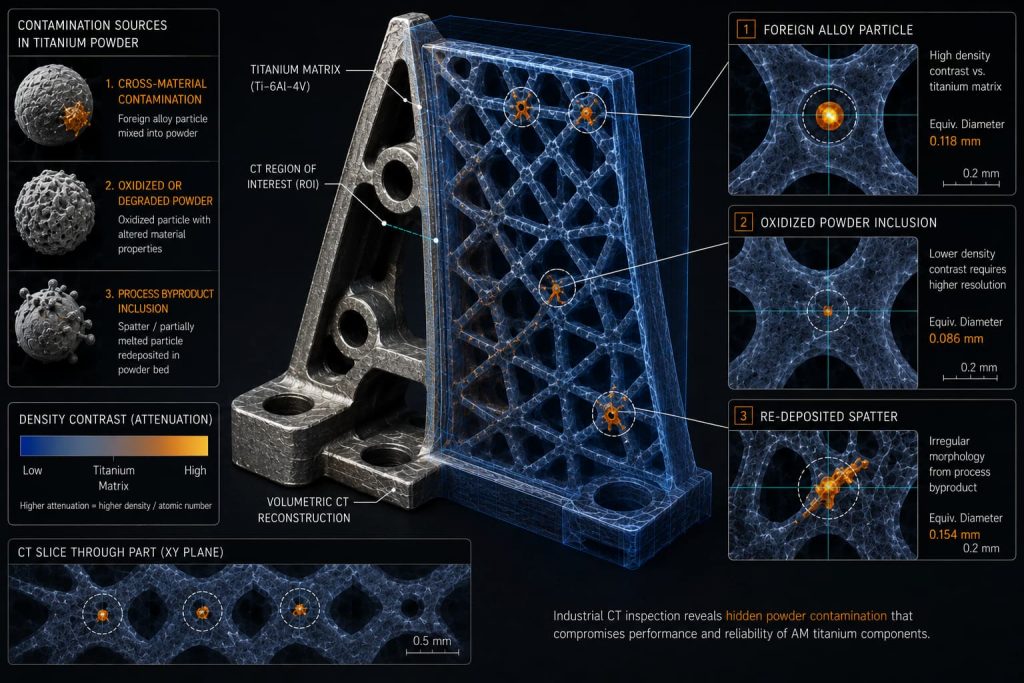
Titanium powder used in additive manufacturing is reused across multiple build cycles. Each reuse cycle is also an opportunity for contamination to enter the powder bed, and once contamination is embedded inside a printed part, it cannot be removed. It can only be found.
3 minutes read
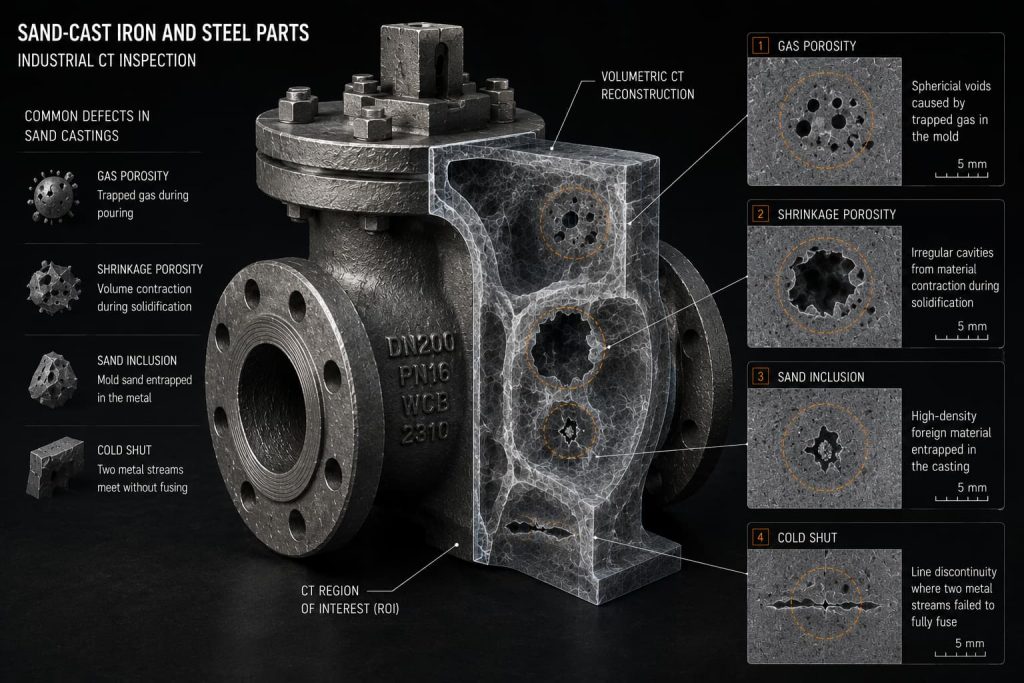
Sand casting CT inspection typically deals with four recurring internal defect categories, shown in the chart above: gas porosity, shrinkage porosity, sand inclusion, and cold shut.
2 minutes read
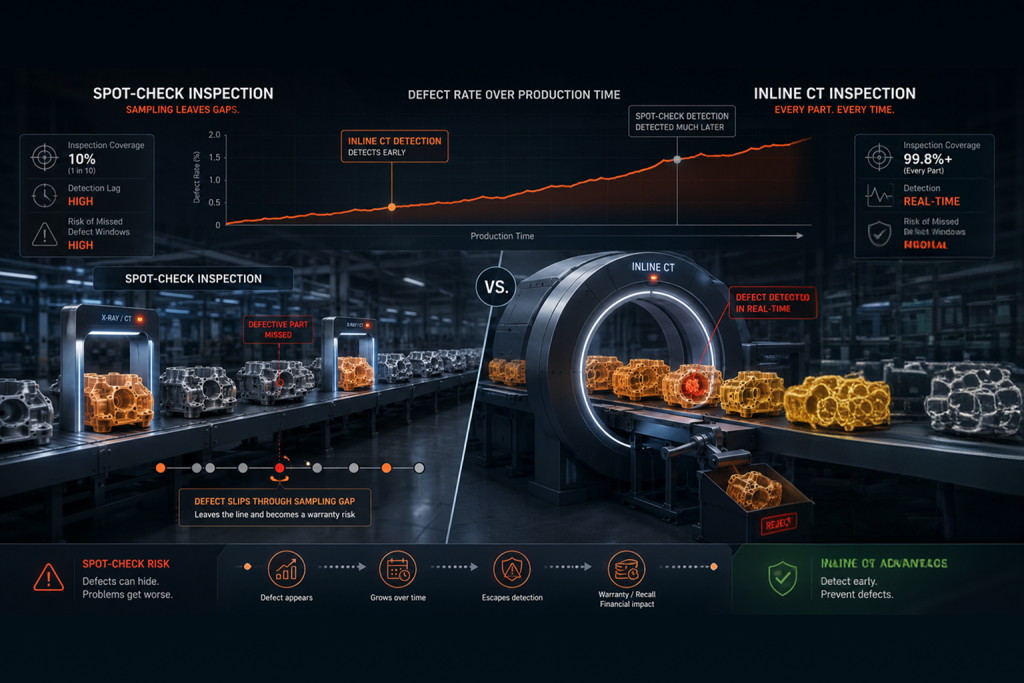
Spot-check inspection has a structural weakness that has nothing to do with the accuracy of the equipment used: it only examines a sample, not every part.
3 minutes read
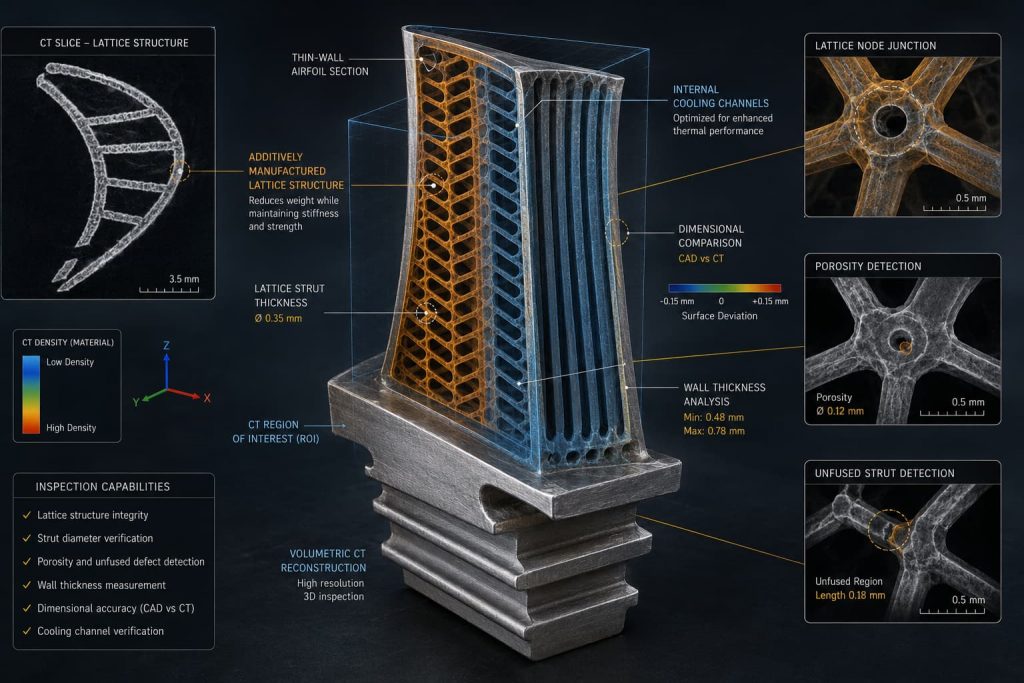
A solid turbine blade scans in a predictable amount of time. An additively manufactured blade with an internal lattice structure, designed for weight reduction and optimized cooling channels, does not.
3 minutes read
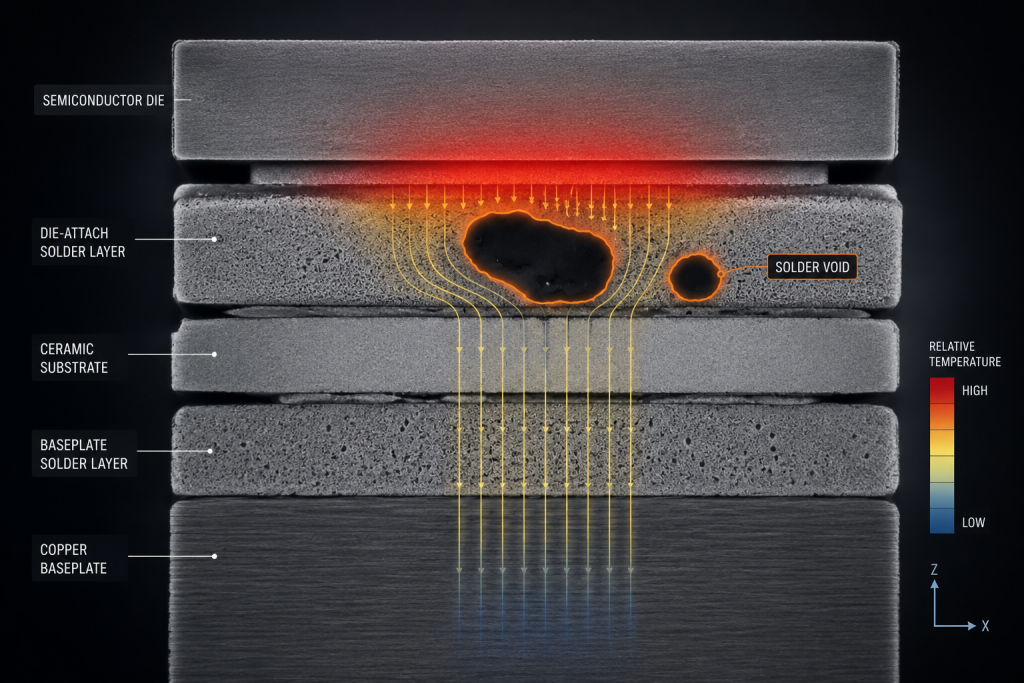
EV power modules convert battery DC to motor-driving AC through IGBT or SiC dies soldered to a ceramic substrate…
3 minutes read
